What 5A05 Aluminum Plate Is and Where It Is Used
5A05 is a wrought aluminum-magnesium alloy of the 5xxx series. Magnesium in the 4.8-5.5% range delivers solid-solution strengthening, while 0.30-0.60% manganese refines the grain structure and raises the recrystallization temperature so that the plate retains useful strength after welding, bending and forming. The alloy is not heat-treatable: strength is developed by strain hardening and then stabilized by annealing, which is why the rolling and annealing sequence decides the final temper.
Because the magnesium content stays below the level at which continuous grain-boundary beta phase becomes a problem, 5A05 behaves well in seawater, salt spray and humid industrial atmospheres. Typical applications include ship superstructures, decks and hull fittings, chemical and water storage tanks, tank-car shells, welded frames, silos and transport structures that combine a corrosive duty with a welded construction.
Composition Window and Standard Basis
Production heats are held inside the composition limits of GB/T 3190 for wrought aluminum alloys. Mechanical property requirements are taken from GB/T 3880.2, dimensional tolerances from GB/T 3880.3, and temper designations follow GB/T 16475. When a buyer works to an ASTM or EN specification, the nearest members of the Al-Mg family are the 5% magnesium grades such as 5056 and EN AW-5083, but the limits are not identical, so the purchase order should always name the grade and temper explicitly.
| Element | Typical limit (wt.%) | Function in the alloy |
|---|---|---|
| Mg | 4.8 - 5.5 | Main strengthener, raises corrosion resistance |
| Mn | 0.30 - 0.60 | Grain refinement, raises recrystallization temperature |
| Si | <= 0.50 | Impurity, limited to protect ductility |
| Fe | <= 0.50 | Impurity, controlled to limit coarse phases |
| Cu | <= 0.10 | Kept low for marine corrosion resistance |
| Zn | <= 0.20 | Kept low to avoid stress corrosion effects |
| Others | each <= 0.05, total <= 0.15 | Residual elements |
| Al | Balance | Matrix |
A workable starting point for plate specification is a density of about 2.65 g/cm3, which lets designers calculate blank weight before the mill order is placed. The reported values should always be confirmed against the certificate issued for the actual heat.
The Production Route from Melt to Finished Plate
Melting and melt treatment. Virgin ingot and clean process scrap are charged in a controlled ratio, then degassed and filtered. Hydrogen and non-metallic inclusions are the main causes of internal porosity in thick plate, so the melt is held within a narrow temperature band and online filtration is used before casting.
Direct-chill casting. The melt is cast into slab ingots with a controlled casting speed and water flow. A fine, uniform grain structure at the slab stage makes the later rolling schedule far easier to control, and it limits the segregation band that would otherwise appear in the final plate.
Homogenizing and scalping. Slabs are held at elevated temperature to dissolve segregated phases and even out the manganese distribution, then both faces are scalped to remove as-cast skin and surface defects.
Hot rolling. The reheated slab is reduced on a reversing mill to transfer, and then on a tandem line to hot-rolled coil or plate. Slab and roll temperatures are tracked at each pass because finishing too cold causes edge cracking and poor through-thickness properties.
Cold rolling. Where a strain-hardened temper or a tight thickness tolerance is required, the hot-rolled material is cold reduced with intermediate annealing steps that restore ductility before the next reduction.
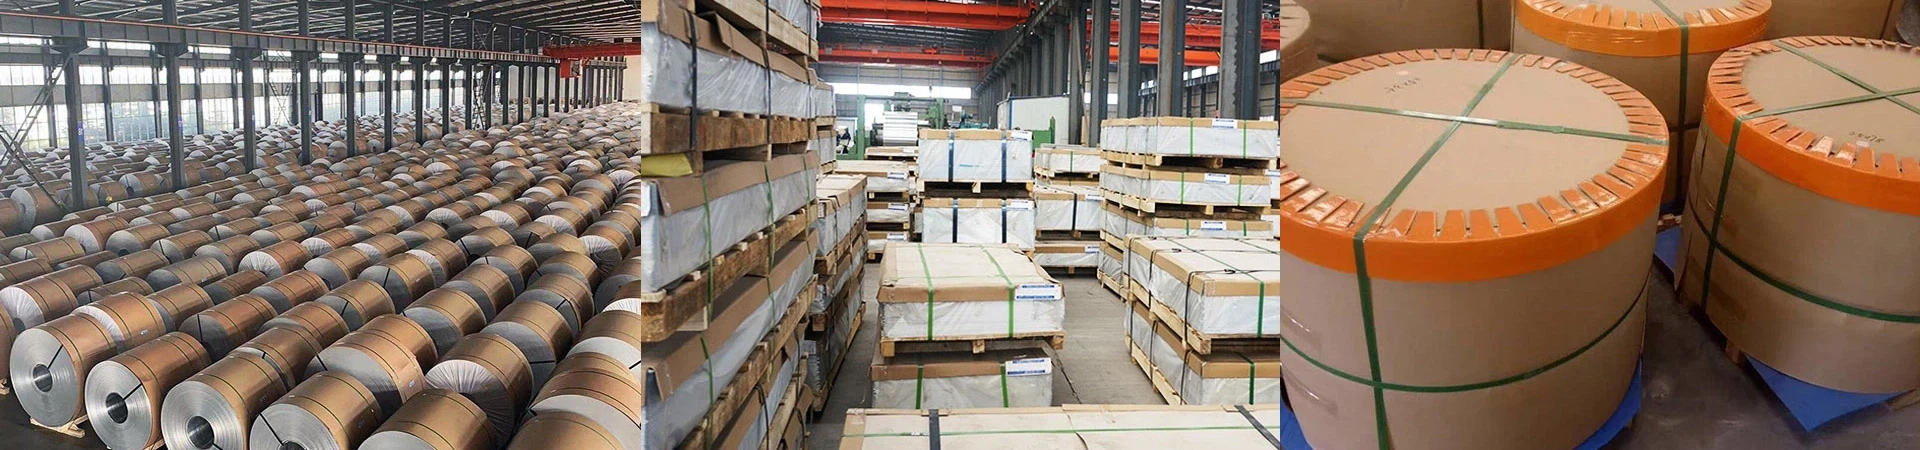
Annealing and finishing. The final anneal sets the temper. Plate is then leveled, edge-trimmed, cut to length or sawed to width, inspected and packed with interleaving and protection against moisture during transport.
Thermal Control Windows
Temperature is the single variable that most often separates a stable 5A05 plate line from one that produces out-of-tolerance material. The windows below are the ranges normally written into the process sheet; the exact figures depend on slab thickness, mill configuration and the required temper.
| Stage | Typical temperature | Purpose |
|---|---|---|
| Homogenizing | 440 - 470 C, several hours | Dissolve segregation, even out Mn |
| Hot rolling start | 400 - 470 C | Low deformation resistance, sound edges |
| Hot rolling finish | above roughly 300 C | Avoid edge cracks and coarse structure |
| Intermediate anneal | 340 - 400 C | Restore ductility between cold passes |
| Final anneal, O temper | 330 - 380 C then air cool | Fully soft, highly formable plate |
| Stabilizing treatment for H tempers | Low temperature, below about 200 C | Improve resistance to stress corrosion |
Two points matter in practice. First, overheating during annealing can coarsen the grain and reduce elongation even though the tensile strength still looks acceptable. Second, the stabilizing treatment used for strain-hardened tempers must be kept below the temperature at which the alloy would start to soften again, otherwise the strength gained by rolling is partly lost.
Quality Control Points that Decide Plate Acceptance
Chemistry per heat. Optical emission spectrometry on a sample from each cast, checked against GB/T 3190 limits before the slab is released to rolling.
Degassing and cleanliness. Hydrogen content and inclusion level monitored to keep porosity out of thick sections.
Temperature logging. Slab, transfer-bar and coil temperatures recorded pass by pass for traceability.
Thickness and flatness. Continuous gauges on the mill plus offline checks against GB/T 3880.3 tolerance tables.
Surface and edges. Roll marks, scratches, inclusions, edge cracks and slivers inspected on both faces under defined lighting.
Mechanical testing. Tensile strength, yield strength and elongation tested per GB/T 3880.2 for the ordered temper.
Corrosion resistance. For welded and long-service marine plate, intergranular corrosion testing such as GB/T 7998 or the nitric acid mass loss method of ASTM G67 gives a direct check on sensitization behavior in the 5xxx series.
Traceability. Heat number and slab number carried through to the finished plate marking so that any deviation can be traced back to the process step that caused it.
Frequently Asked Questions
Q: Is 5A05 a heat-treatable alloy?
No. 5A05 belongs to the non-heat-treatable 5xxx series. Its strength comes from magnesium in solid solution plus strain hardening, and annealing is used to soften the material for forming. That is also why temper designations are based on H and O conditions rather than T conditions.
Q: What is the most common cause of poor weld quality in 5A05 plate?
Surface contamination and excessive heat input are the usual causes. The oxide film must be removed mechanically or chemically just before welding, filler selection must match the alloy, and heat input should be kept low enough to avoid a wide softened zone and hot cracking in restrained joints.
Q: How does 5A05 compare with 5083 and 5056?
All three are Al-Mg alloys with roughly 5% magnesium. 5A05 balances strength, formability and weldability for general marine and tank work, while 5083 is used where higher strength and better weld toughness are needed and 5056 is chosen when a higher magnesium content and finer surface finish are wanted.
Q: Can 5A05 plate be cold formed after the final anneal?
Yes, in the O temper the plate has good ductility and can be bent, rolled and deep formed. Forming direction relative to the rolling direction should be respected, bend radii should not be tighter than the gauge-based minimum, and heavily formed parts should be annealed again before service in a corrosive environment.
Q: Why does the spec often require manganese in the alloy?
Manganese refines the cast grain structure, slows recrystallization during hot rolling and improves strength slightly without hurting corrosion resistance. Combined with a controlled homogenizing cycle it produces a plate with a more uniform grain size through the thickness, which improves fatigue and forming behavior.
Q: Which plate thicknesses are normally supplied?
Sheet and plate are supplied from thin gauges up to heavy plate, with thickness, width and length agreed against GB/T 3880.3 tolerances. Heavy plate is normally supplied in the O or as-rolled condition, while thinner gauges can be supplied in a range of strain-hardened tempers depending on the strength and formability needed.